A foundry website should answer the questions an OEM buyer or engineer asks before they send a pattern package: what alloys and processes you pour, what casting sizes and weights you hold, what finishing and machining you offer in-house or as a controlled handoff, how you inspect, and how quotes move. Put those facts in plain text on pages you own. That is the marketing. Design is the layout that makes those facts easy to find on a phone and easy for search and AI to cite.
Dramatic pour videos and the word “heritage” do not win the award by themselves. Alloy lists, process pages, and a clean RFQ path do.
Who is reading the site
Most serious foundry traffic is a purchasing lead, a design engineer converting a weldment to cast, or a quality manager comparing suppliers. They already have a geometry, an alloy callout, and a volume target. They are checking whether your pour and handoff match the job without a long plant tour first.
They search and ask AI things like ductile iron foundry Midwest, aluminum sand casting with machining, investment casting Iowa, or casting-to-machine handoff for ag parts. Your website has to match that language with real process and alloy facts — not agency adjectives.
Iowa and Midwest foundries near the ag and industrial OEM corridor compete the same way: prove alloy and size envelope, then make the quote path short.
What the homepage has to say in the first screen
In plain HTML text, not locked in a logo:
1. Foundry name and city (or plants) 2. Core processes: sand, investment, permanent mold, ductile, aluminum — only what you actually pour 3. Phone and email that reach a human who quotes 4. One clear button: Request a quote / Submit casting RFQ 5. One line on machining/finishing handoff if you offer it
If someone lands from Google, LinkedIn, or an AI answer and cannot find those five things in ten seconds, the rest of the brand story does not matter.
Build capability pages, not a keyword dump
One URL should equal one clear capability. Examples that work for foundries of different sizes:
- Alloys — ductile iron grades, gray iron, aluminum, steel — only what you pour
- Processes — green sand, no-bake, investment, permanent mold
- Size and weight envelope — typical and max
- Finishing and machining — grind, heat treat partners, in-house CNC handoff
- Quality — spectro, dimensional, hardness, FAIR when real
- File formats and tooling — how you take CAD, pattern, and tooling responsibility
A thin “Casting solutions” page that lists every buzzword is worse than three honest pages. Search and AI cite specific files. Buyers save specific pages for the RFQ folder.
Smaller foundries can start with one strong alloys-and-process page — then split as content grows. Foundries with both pour and machine shops should give the machining handoff its own URL. Buyers search that path on purpose.
Calm casting proof beats vague “liquid metal craft”
Publish the plant the way a buyer audits a supplier:
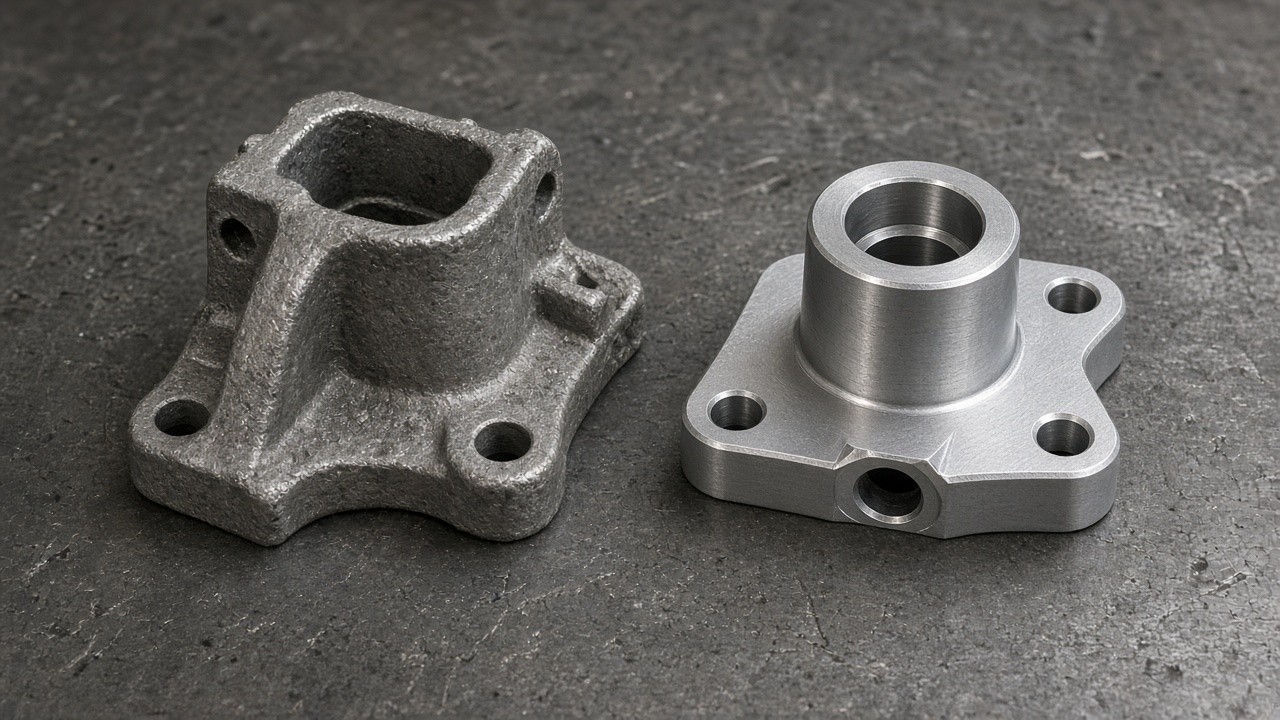
- Photos comparing as-cast and machined finish when you do both
- Alloy and process lists with honest envelopes
- Typical lead times for tooling and production
- Pattern and tooling ownership notes
Stock “sparks and glory” heroes without alloy facts hurt trust. You do not need a cinematic pour on day one. You do need numbers and a true process map.
The RFQ path is the conversion
Marketing for a foundry is not a brochure request first. It is a quote.
A good RFQ page or form asks for:
- Company and corporate email
- Alloy and process needed
- Annual volume and sample quantity
- Machining / finishing requirements
- Secure upload for CAD and drawings
- Tooling status (existing pattern vs new)
- Stated quote response window you can keep
If the only CTA is “Contact us” with a blank message box, engineers bounce and send the package to the foundry whose form already matches their checklist.
Content that feeds search and AI without theater
Useful posts and pages look like work notes, not slogans:
- When to cast vs fab a part
- What to send with a casting RFQ
- How casting-to-machine handoff should be documented
- Short job write-ups: alloy, process, industry — no customer secrets
- Midwest OEM notes for ag and industrial buyers
Your website stays the source of record. Directories, LinkedIn, and Google Business can point back to these pages. Do not bury the only true alloy list inside a PDF brochure that crawlers and chat tools skip.
Bots already do a large share of web requests. People still buy castings. Machines increasingly decide which foundry they mention first. Plain-text capabilities on a domain you own are how you stay in that short list.
Design rules that fit a foundry brand
- Fast on mobile. Buyers open links between meetings.
- High-contrast text. No pale gray on gray.
- Navigation: Alloys / Processes, Machining handoff, Quality, RFQ, About, Contact
- Phone click-to-call in the header
- No fake OEM logos
- You own the domain, hosting accounts, and content when the agency relationship ends
Pretty is fine after the facts are readable. Pretty instead of facts is a stalled quote queue.
What Upley does for shops like this
Upley builds and hosts websites for Iowa and Midwest service and manufacturing businesses. For a foundry that means clear alloy and process pages, an RFQ path that matches how OEM buyers actually buy, hosting that stays up for daily crawls, and a way to publish real casting and machined-finish photos without turning your metallurgists into marketers.
Same Iowa web team that ran Big Ten Web Design — design, hosting, SEO — plus the modern layer so search and AI can find the true file about your pours and handoffs.
If you pour metal and your current site still says “foundry excellence” with no alloy list, start with the homepage five facts and one honest capabilities page. Then grow from the RFQ.
Book 30 minutes: /half-hour-meeting/ Call 319-535-2508 · aaron@upley.com Iowa City, Cedar Rapids, Quad Cities / Davenport